
Introduction to Oil Water Separator
An oil water separator is a device designed to separate oil and water mixtures. It plays a crucial role in various industries such as manufacturing, oil and gas, maritime, and wastewater treatment. The separation process is based on the difference in density between oil and water, as well as other physical properties. By effectively separating oil from water, it helps to meet environmental regulations, protect water resources, and prevent pollution. There are different types of oil water separators, including gravity separators, coalescing separators, centrifugal separators, and membrane separators, each with its own working principle and application scenarios.
10 Top Oil Water Separator Manufacturers
1. Jinhua Shenzhou Centrifuge Co., Ltd.
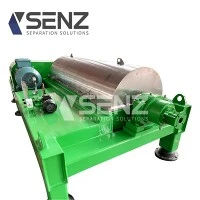
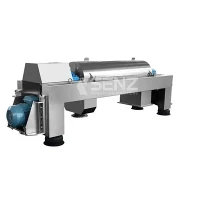
Jinhua Shenzhou Centrifuge Co., Ltd. is a leading manufacturer in the field of separation equipment, with a particular focus on oil water separators. The company has a long - standing history of research, development, and production, and is committed to providing high - quality and efficient separation solutions.
Company OverviewEstablished in [year of establishment], Jinhua Shenzhou Centrifuge Co., Ltd. has grown from a small - scale enterprise to a well - known company in the separation industry. It has a modern production base equipped with advanced manufacturing equipment and a professional R & D team. The company adheres to strict quality control standards and has obtained various international certifications, which ensures the reliability and performance of its products.
Oil Water Separator Features
- High - efficiency Separation: The oil water separators produced by Jinhua Shenzhou Centrifuge Co., Ltd. are based on advanced centrifugal separation technology. The centrifugal force generated by the high - speed rotation of the centrifuge can quickly and effectively separate oil and water, achieving a high degree of separation efficiency. For example, in industrial wastewater treatment, it can reduce the oil content in water to a very low level, meeting the strictest environmental discharge standards.
- Customization: The company understands that different industries have different requirements for oil water separators. Therefore, it offers customized solutions. Whether it is a small - scale laboratory application or a large - scale industrial production line, the company can design and manufacture oil water separators according to the specific needs of customers, including the size, capacity, and separation performance of the equipment.
- Durable and Reliable: The materials used in the production of oil water separators are of high quality, which ensures the durability of the equipment. The company also pays attention to the design and manufacturing process to improve the reliability of the equipment. With proper maintenance, the oil water separators can operate stably for a long time, reducing the cost of equipment replacement and maintenance for customers.
Company Advantages
- Technical Innovation: Jinhua Shenzhou Centrifuge Co., Ltd. invests a large amount of resources in research and development every year. The R & D team is constantly exploring new separation technologies and improving the performance of existing products. This continuous innovation enables the company to keep up with the latest trends in the industry and provide customers with more advanced and efficient oil water separation solutions.
- Excellent After - sales Service: The company has a professional after - sales service team that can provide timely and comprehensive after - sales support. Whether it is equipment installation, debugging, maintenance, or technical consultation, the after - sales service team can respond quickly and solve problems for customers. This high - quality after - sales service has won the trust and praise of customers.
- Competitive Pricing: Despite the high - quality products and services, Jinhua Shenzhou Centrifuge Co., Ltd. offers competitive prices. By optimizing the production process and supply chain management, the company can reduce production costs and transfer the cost savings to customers, providing customers with cost - effective oil water separation solutions.
Website: https://www.senz-separation.com/
2. Alfa Laval
Company OverviewAlfa Laval is a global leader in heat transfer, separation, and fluid handling technology. With a history dating back to 1883, the company has a strong reputation for innovation and quality. It operates in more than 100 countries and has a wide range of products and services. Alfa Laval's oil water separators are used in various industries, including marine, oil and gas, and food and beverage.
Oil Water Separator Features
- Advanced Coalescing Technology: Alfa Laval's oil water separators use advanced coalescing technology. The coalescing media in the separator can cause small oil droplets to combine into larger ones, which are then more easily separated from the water. This technology ensures high - efficiency separation even for emulsified oil - water mixtures.
- Compact Design: The company's oil water separators are designed to be compact, which is especially beneficial for applications where space is limited. For example, in marine vessels, the compact design allows for easy installation in the limited engine room space.
- Automated Operation: Many of Alfa Laval's oil water separators are equipped with automated control systems. These systems can monitor the separation process in real - time, adjust the operating parameters automatically, and provide alarm signals in case of abnormal conditions. This automation reduces the need for manual intervention and improves the reliability of the separation process.
Company Advantages
- Global Presence: With its extensive global network, Alfa Laval can provide local support to customers around the world. Whether it is product sales, installation, or after - sales service, customers can easily access the company's resources in their region.
- Strong R & D Capability: The company invests heavily in research and development. Its R & D team is constantly working on improving the performance of oil water separators, developing new materials and technologies, and adapting to the changing needs of different industries.
- Industry Experience: Alfa Laval has more than a century of experience in the separation industry. This long - term experience has enabled the company to understand the unique requirements of different industries and develop customized solutions accordingly.
3. Pall Corporation
Company OverviewPall Corporation is a leading provider of filtration, separation, and purification solutions. It has a global presence and serves a wide range of industries, including aerospace, biotechnology, and industrial manufacturing. The company's oil water separators are known for their high - performance filtration and separation capabilities.
Oil Water Separator Features
- High - performance Filtration Media: Pall Corporation uses high - quality filtration media in its oil water separators. These media can effectively remove fine oil droplets and solid particles from the water, achieving a high level of water purity. The filtration media are also designed to have a long service life, reducing the frequency of media replacement.
- Modular Design: The oil water separators have a modular design, which allows for easy expansion and customization. Customers can add or remove modules according to their changing production needs, making the equipment more flexible and adaptable.
- Low - maintenance Operation: The design of Pall Corporation's oil water separators focuses on reducing maintenance requirements. The equipment is easy to clean and maintain, and the replacement of filter elements can be carried out quickly and easily, minimizing downtime.
Company Advantages
- Filtration Expertise: As a company with a strong focus on filtration technology, Pall Corporation has in - depth expertise in this field. This expertise enables the company to develop oil water separators with superior filtration performance and reliability.
- Customer - centric Approach: The company places a high emphasis on customer satisfaction. It works closely with customers to understand their specific needs and provides customized solutions. The company also offers comprehensive technical support and training to help customers make the most of their oil water separators.
- Quality Assurance: Pall Corporation has a strict quality control system in place. All products are tested and verified to meet the highest quality standards before leaving the factory. This ensures that customers receive reliable and high - performance oil water separators.
4. Andritz AG
Company OverviewAndritz AG is an international technology group that provides plants, equipment, and services for various industries, including pulp and paper, metal processing, and water treatment. The company's oil water separators are part of its comprehensive water treatment solutions.
Oil Water Separator Features
- Integrated Solutions: Andritz offers integrated oil water separation solutions that combine different separation technologies. For example, it may use a combination of gravity separation, coalescence, and filtration to achieve the best separation results. This integrated approach can handle complex oil - water mixtures more effectively.
- Energy - efficient Design: The oil water separators are designed with energy efficiency in mind. The company uses advanced hydraulic and mechanical designs to reduce energy consumption during the separation process. This not only helps to lower operating costs for customers but also contributes to environmental protection.
- Robust Construction: Andritz's oil water separators are built with robust construction. The equipment is made of high - quality materials that can withstand harsh operating conditions, such as high pressure, high temperature, and corrosive environments.
Company Advantages
- Comprehensive Product Portfolio: Andritz has a wide range of products and services in the water treatment field. This allows the company to provide customers with one - stop solutions for their oil water separation needs. Customers can also benefit from the synergy between different products and services.
- Engineering Expertise: The company has a team of experienced engineers who can design and optimize oil water separation systems according to the specific requirements of customers. Their engineering expertise ensures the efficient and reliable operation of the equipment.
- Global Service Network: Andritz has a global service network that can provide timely maintenance and repair services. This network ensures that customers can get support whenever and wherever they need it.
5. GEA Group
Company OverviewGEA Group is a global technology company that specializes in process engineering and equipment for the food, beverage, and pharmaceutical industries, as well as other industrial sectors. The company's oil water separators are designed to meet the strict hygiene and quality requirements of these industries.
Oil Water Separator Features
- Hygienic Design: GEA's oil water separators are designed with a focus on hygiene. The equipment is made of materials that are easy to clean and sterilize, and the design minimizes the risk of bacteria growth and contamination. This is especially important for industries such as food and beverage, where product safety is of utmost importance.
- Precise Separation Control: The company's oil water separators are equipped with advanced control systems that can precisely control the separation process. These systems can adjust the operating parameters according to the characteristics of the oil - water mixture, ensuring consistent and high - quality separation results.
- Scalability: GEA's oil water separators are scalable, which means that they can be easily adjusted to handle different production volumes. Whether it is a small - scale production line or a large - scale industrial plant, the equipment can be configured to meet the specific needs of the customer.
Company Advantages
- Industry - specific Knowledge: GEA has in - depth knowledge of the industries it serves. This allows the company to develop oil water separators that are specifically tailored to the requirements of each industry. For example, in the food industry, the equipment is designed to meet strict food safety regulations.
- Innovation and Technology Leadership: The company is at the forefront of innovation in the process engineering field. It continuously invests in research and development to improve the performance of its oil water separators and introduce new technologies.
- Strong Customer Relationships: GEA has built strong relationships with its customers over the years. The company provides excellent customer service, from product design and installation to after - sales support. This customer - centric approach has helped the company to maintain a high level of customer satisfaction.
6. Siemens Water Technologies
Company OverviewSiemens Water Technologies is a division of Siemens AG, a global technology powerhouse. The company offers a wide range of water treatment solutions, including oil water separators. It combines advanced technology with reliable engineering to provide customers with efficient and sustainable water treatment solutions.
Oil Water Separator Features
- Smart Monitoring and Control: Siemens' oil water separators are equipped with smart monitoring and control systems. These systems can collect real - time data on the separation process, such as oil content, flow rate, and pressure. The data can be analyzed to optimize the operating parameters and predict potential problems, enabling proactive maintenance.
- Integration with Digital Solutions: The company integrates its oil water separators with digital solutions, such as the Internet of Things (IoT) and cloud computing. This allows for remote monitoring and control of the equipment, as well as data sharing and analysis across different locations.
- Sustainable Design: Siemens focuses on sustainable design in its oil water separators. The equipment is designed to minimize energy consumption, reduce waste, and use environmentally friendly materials. This not only helps to protect the environment but also reduces the operating costs for customers.
Company Advantages
- Digitalization Expertise: As a leader in digital technology, Siemens has extensive expertise in digitalizing industrial processes. This expertise enables the company to develop oil water separators with advanced digital features, improving the efficiency and reliability of the separation process.
- Global R & D and Manufacturing Network: Siemens has a global R & D and manufacturing network, which allows it to quickly respond to the changing needs of customers around the world. The company can also leverage its global resources to develop and produce high - quality oil water separators.
- Comprehensive Service Portfolio: The company offers a comprehensive service portfolio, including installation, commissioning, maintenance, and upgrade services. This ensures that customers can get all - round support for their oil water separators throughout the equipment's lifecycle.
7. Sulzer
Company OverviewSulzer is a global leader in fluid engineering. The company provides a wide range of products and services, including pumps, mixers, and separators. Its oil water separators are known for their high - performance and reliability in various industries, such as oil and gas, power generation, and chemical processing.
Oil Water Separator Features
- High - speed Centrifugal Separation: Sulzer's oil water separators use high - speed centrifugal technology. The high - speed rotation of the centrifuge can generate a strong centrifugal force, which can quickly separate oil and water. This technology is particularly effective for separating high - viscosity oil - water mixtures.
- Self - cleaning Function: Some of Sulzer's oil water separators are equipped with a self - cleaning function. The equipment can automatically clean the separation chamber and remove the accumulated oil and solids, reducing the need for manual cleaning and maintenance.
- Corrosion - resistant Materials: The company uses corrosion - resistant materials in the construction of its oil water separators. This ensures that the equipment can withstand the corrosive effects of oil and water, especially in harsh industrial environments.
Company Advantages
- Fluid Engineering Expertise: Sulzer has a long - standing reputation in fluid engineering. Its expertise in this field allows the company to design and manufacture oil water separators with excellent fluid handling capabilities, ensuring efficient and stable operation.
- Customized Solutions: Sulzer understands that different industries have different requirements for oil water separators. The company offers customized solutions based on the specific needs of customers, including the design, capacity, and performance of the equipment.
- Global Service and Support: Sulzer has a global service and support network. The company can provide timely maintenance, repair, and spare parts services to customers around the world, minimizing downtime and ensuring the continuous operation of the equipment.
8. Hiller GmbH
Company OverviewHiller GmbH is a German company that specializes in the production of centrifuge technology. With a history of more than 100 years, the company has a deep understanding of separation technology and has developed a wide range of oil water separators for different applications.
Oil Water Separator Features
- High - precision Separation: Hiller's oil water separators are known for their high - precision separation capabilities. The company uses advanced centrifuge design and control technology to ensure that the oil and water are separated with high accuracy, even for very fine oil droplets.
- Energy - saving Design: The oil water separators are designed to be energy - saving. The company optimizes the centrifuge design and operating parameters to reduce energy consumption during the separation process, which helps to lower the operating costs for customers.
- Long - term Reliability: Hiller's products are built with high - quality materials and strict manufacturing processes. The oil water separators are designed to have a long service life and can operate reliably under continuous use.
Company Advantages
- German Engineering Excellence: As a German company, Hiller is known for its engineering excellence. The company adheres to strict quality standards and uses advanced manufacturing techniques to produce high - quality oil water separators.
- Continuous Innovation: Hiller invests in research and development to continuously improve its products. The company is constantly exploring new technologies and materials to enhance the performance of its oil water separators.
- Customer - oriented Service: The company provides customer - oriented service. It works closely with customers to understand their needs and provides customized solutions and technical support.
9. Weir Group
Company OverviewWeir Group is a global engineering company that provides solutions for the mining, oil and gas, and power industries. The company's oil water separators are designed to meet the harsh operating conditions of these industries.
Oil Water Separator Features
- Robust and Durable Design: Weir Group's oil water separators are built with a robust and durable design. The equipment is made of high - strength materials that can withstand high pressure, high temperature, and abrasive environments. This makes the separators suitable for use in industries such as mining and oil and gas.
- High - capacity Separation: The company's oil water separators are capable of handling large volumes of oil - water mixtures. They are designed with high - capacity separation chambers and efficient separation mechanisms to ensure fast and effective separation.
- Adaptability to Harsh Environments: The oil water separators are designed to be adaptable to harsh environments. They can operate in extreme temperatures, high humidity, and dusty conditions, ensuring reliable performance in various industrial settings.
Company Advantages
- Industry - specific Experience: Weir Group has extensive experience in serving the mining, oil and gas, and power industries. This experience allows the company to understand the unique requirements of these industries and develop oil water separators that are specifically tailored to their needs.
- Global Support Network: The company has a global support network that can provide timely service and support to customers around the world. Whether it is installation, maintenance, or repair, customers can rely on Weir Group's local teams for assistance.
- Innovation in Engineering: Weir Group is committed to innovation in engineering. The company invests in research and development to improve the performance of its oil water separators and introduce new technologies to meet the changing needs of the industries it serves.
10. Evoqua Water Technologies
Company OverviewEvoqua Water Technologies is a leading provider of water and wastewater treatment solutions. The company offers a comprehensive range of products and services, including oil water separators. It serves a variety of industries, such as municipal, industrial, and commercial.
Oil Water Separator Features
- Comprehensive Treatment Solutions: Evoqua's oil water separators are part of its comprehensive water treatment solutions. The company can combine the oil water separators with other treatment processes, such as filtration, disinfection, and biological treatment, to provide a complete water treatment solution.
- Advanced Monitoring and Reporting: The oil water separators are equipped with advanced monitoring and reporting systems. These systems can monitor the performance of the separator in real - time, generate reports on the separation efficiency and water quality, and provide alerts in case of any abnormal conditions.
- Compliance with Regulations: Evoqua's oil water separators are designed to comply with various environmental regulations. The company ensures that the equipment can effectively remove oil from water to meet the discharge standards set by local and international authorities.
Company Advantages
- Water Treatment Expertise: Evoqua has in - depth expertise in water treatment. This expertise allows the company to develop oil water separators that are not only effective in separating oil and water but also integrated into a comprehensive water treatment system.
- Regulatory Compliance Support: The company provides support to customers in ensuring regulatory compliance. It helps customers understand the relevant regulations and provides solutions to meet these requirements, reducing the legal risks for customers.
- Customer - focused Approach: Evoqua takes a customer - focused approach. It works closely with customers to understand their specific water treatment needs and provides customized solutions and support throughout the project lifecycle.
Conclusion
The 10 oil water separator manufacturers mentioned above are all leaders in the global market, each with its own unique features and advantages. Jinhua Shenzhou Centrifuge Co., Ltd. stands out with its high - efficiency centrifugal separation technology, customization capabilities, and excellent after - sales service. Alfa Laval is known for its advanced coalescing technology and global presence. Pall Corporation offers high - performance filtration media and a modular design. Andritz provides integrated solutions and energy - efficient designs. GEA Group focuses on hygienic design and precise separation control. Siemens Water Technologies combines digital solutions with sustainable design. Sulzer has high - speed centrifugal separation and self - cleaning functions. Hiller GmbH offers high - precision separation and German engineering excellence. Weir Group provides robust and durable designs for harsh environments. Evoqua Water Technologies offers comprehensive treatment solutions and regulatory compliance support.
In the future, as environmental regulations become more stringent and the demand for efficient oil water separation increases, these manufacturers will continue to play an important role in the market. They will likely invest more in research and development to further improve the performance of their oil water separators, develop new technologies, and provide more sustainable and cost - effective solutions to meet the evolving needs of customers.