
Introduction to Oil Water Separators
Oil water separators are essential devices used in various industries to separate oil and water mixtures. These separators play a crucial role in environmental protection, as they prevent oil from contaminating water sources. They are widely used in industries such as manufacturing, automotive, oil and gas, and food processing. The principle behind oil water separators is based on the difference in density between oil and water. By allowing the mixture to settle, the oil rises to the top while the water remains at the bottom, and then the two can be separated. There are different types of oil water separators, including gravity separators, coalescing separators, and centrifugal separators, each with its own advantages and applications.
1. Jinhua Shenzhou Centrifuge Co., Ltd.
Company Introduction
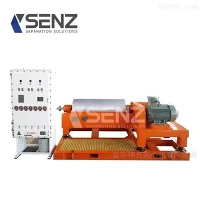
Jinhua Shenzhou Centrifuge Co., Ltd. is a leading manufacturer in the field of separation equipment, with a strong focus on oil water separation technology. The company has a long - standing history of innovation and quality production. It is equipped with advanced production facilities and a team of highly skilled engineers and technicians. They are committed to providing high - performance and reliable oil water separators to meet the diverse needs of customers around the world.
The company's research and development department is constantly working on improving the efficiency and performance of their products. They conduct in - depth research on different separation mechanisms and materials to develop more effective oil water separation solutions. Jinhua Shenzhou Centrifuge Co., Ltd. also places great emphasis on quality control. Every product undergoes strict testing and inspection before leaving the factory to ensure that it meets international quality standards.
Features and Advantages in Oil Water Separation
- High - efficiency Separation: Their centrifugal oil water separators use advanced centrifugal technology to achieve rapid and efficient separation of oil and water. The high - speed rotation of the centrifuge creates a strong centrifugal force, which can quickly separate the oil from the water, even for emulsified oil - water mixtures.
- Customization: The company offers customized solutions according to the specific requirements of customers. Whether it is the capacity, size, or specific separation performance, they can design and manufacture oil water separators that meet the unique needs of different industries.
- Reliability: With high - quality materials and precise manufacturing processes, their products are known for their reliability and long service life. They can operate stably in harsh industrial environments, reducing the frequency of maintenance and replacement.
- Environmental - friendly: The separators are designed to minimize the environmental impact. They can effectively remove oil from water, ensuring that the discharged water meets environmental standards, which is in line with the global trend of environmental protection.
Website: https://www.senz-separation.com/
2. Alfa Laval
Company Introduction
Alfa Laval is a well - known global company with a rich history dating back to the 19th century. It is a leading provider of specialized products and engineering solutions in the areas of heat transfer, separation, and fluid handling. The company has a vast global presence, with offices and production facilities in multiple countries.
Alfa Laval's R & D efforts are focused on developing cutting - edge technologies to improve the performance of their products. They invest heavily in research to stay ahead in the market. Their manufacturing processes are highly automated and precise, ensuring the quality and consistency of their products.
Features and Advantages in Oil Water Separation
- Advanced Coalescing Technology: Alfa Laval's oil water separators use advanced coalescing technology. Coalescers are designed to combine small oil droplets into larger ones, making it easier to separate the oil from the water. This technology significantly improves the separation efficiency, especially for fine oil droplets.
- Wide Range of Applications: Their products are suitable for a wide range of industries, including marine, oil and gas, and industrial manufacturing. They can handle different types of oil - water mixtures, from light oils to heavy crude oils.
- Energy - efficient Design: The company is committed to energy - saving solutions. Their oil water separators are designed to consume less energy while achieving high - performance separation. This not only reduces operating costs for customers but also contributes to environmental protection.
- Global Support Network: With a global network of service centers, Alfa Laval can provide prompt and efficient after - sales service. Customers can get technical support, spare parts, and maintenance services in a timely manner, ensuring the continuous operation of their oil water separators.
3. Andritz
Company Introduction
Andritz is a large - scale international technology group that offers a wide range of products and services in the fields of hydropower, pulp and paper, metals, and separation technology. In the area of oil water separation, Andritz has a strong reputation.
The company has a comprehensive R & D system that focuses on developing innovative separation technologies. They collaborate with research institutions and universities to stay at the forefront of technological advancements. Andritz's manufacturing facilities are equipped with state - of - the - art equipment, enabling them to produce high - quality oil water separators.
Features and Advantages in Oil Water Separation
- Integrated Solutions: Andritz provides integrated oil water separation solutions. They not only offer the separators themselves but also related equipment and systems, such as pre - treatment units and control systems. This integrated approach ensures a more efficient and seamless separation process.
- High - Capacity Separation: Their separators are designed to handle large - volume oil - water mixtures. This makes them suitable for industries with high - throughput requirements, such as refineries and large - scale manufacturing plants.
- Robust Construction: The oil water separators are built with high - quality materials and a robust design. They can withstand harsh operating conditions, including high pressures and temperatures, ensuring long - term reliable operation.
- Process Optimization: Andritz offers process optimization services. Their experts can analyze the customer's specific separation process and make adjustments to improve the efficiency and performance of the oil water separator, reducing operating costs and waste.
4. Pall Corporation
Company Introduction
Pall Corporation is a global leader in filtration, separation, and purification technologies. The company has a long - standing history of providing high - quality filtration products and solutions. In the field of oil water separation, Pall has developed a range of advanced products.
Pall's R & D team is constantly exploring new materials and technologies for filtration and separation. They have a deep understanding of the physical and chemical properties of different substances, which allows them to design more effective oil water separation solutions. The company also has a strong quality management system to ensure the reliability of its products.
Features and Advantages in Oil Water Separation
- Advanced Filtration Media: Pall uses advanced filtration media in its oil water separators. These media have high - efficiency filtration capabilities, which can effectively remove fine oil droplets and impurities from the water. The media are also designed to have a long service life, reducing the frequency of replacement.
- Modular Design: Their oil water separators have a modular design, which allows for easy installation, expansion, and maintenance. Customers can customize the system according to their specific needs by adding or removing modules.
- Compliance with Standards: Pall's products comply with various international standards and regulations. This ensures that the separated water meets the required environmental and quality standards, which is crucial for industries that need to meet strict regulatory requirements.
- Technical Expertise: The company has a team of technical experts who can provide in - depth technical support and advice to customers. They can help customers select the most suitable oil water separator for their specific applications and provide training on the operation and maintenance of the equipment.
5. Parker Hannifin
Company Introduction
Parker Hannifin is a diversified global manufacturer of motion and control technologies and systems. In the area of oil water separation, the company offers a range of products and solutions.
Parker Hannifin has a strong R & D focus on developing new and improved separation technologies. They invest in research to enhance the performance and efficiency of their oil water separators. The company also has a global manufacturing and distribution network, ensuring that its products are readily available to customers around the world.
Features and Advantages in Oil Water Separation
- Innovative Design: Parker Hannifin's oil water separators feature innovative designs. For example, some of their products use unique flow - control mechanisms to improve the separation efficiency. These designs are based on in - depth research and engineering expertise.
- Versatile Applications: Their products can be used in a variety of industries, including automotive, aerospace, and industrial manufacturing. They can handle different types of oil - water mixtures, from light lubricating oils to heavy industrial oils.
- High - Quality Components: The company uses high - quality components in its oil water separators. This ensures the reliability and durability of the products, reducing the risk of breakdowns and downtime.
- System Integration: Parker Hannifin can integrate its oil water separators into larger systems. This allows for seamless operation and better control of the overall separation process, especially in complex industrial environments.
6. Siemens
Company Introduction
Siemens is a global powerhouse in the fields of electrification, automation, and digitalization. In the area of oil water separation, Siemens offers advanced solutions that combine its expertise in automation and control with separation technology.
Siemens has a large - scale R & D infrastructure that focuses on developing intelligent and efficient separation systems. They use digital technologies such as sensors, data analytics, and artificial intelligence to optimize the performance of their oil water separators. The company's manufacturing facilities are known for their high - precision production and quality control.
Features and Advantages in Oil Water Separation
- Intelligent Control Systems: Siemens' oil water separators are equipped with intelligent control systems. These systems can monitor the separation process in real - time, adjust the operating parameters automatically, and provide early warnings of potential problems. This improves the efficiency and reliability of the separation process.
- Digital Twin Technology: The company uses digital twin technology to simulate and optimize the performance of the oil water separator. This allows for better design and operation of the system, reducing energy consumption and improving separation efficiency.
- Integration with Industrial IoT: Siemens' solutions can be integrated with the Industrial Internet of Things (IIoT). This enables remote monitoring and control of the oil water separator, as well as data - driven decision - making for process optimization.
- Comprehensive Service Portfolio: Siemens offers a comprehensive service portfolio, including installation, commissioning, maintenance, and upgrade services. Their global service network ensures that customers can get timely support wherever they are.
7. Sulzer
Company Introduction
Sulzer is a global leader in fluid engineering. The company provides a wide range of products and services in the areas of pumps, separators, and mixing technology. In the field of oil water separation, Sulzer has a strong presence.
Sulzer's R & D efforts are focused on improving the performance and efficiency of its separation products. They conduct extensive research on fluid dynamics and separation mechanisms to develop more effective oil water separation solutions. The company's manufacturing facilities are equipped with advanced machinery and technology, ensuring high - quality production.
Features and Advantages in Oil Water Separation
- Advanced Fluid Dynamics Design: Sulzer's oil water separators are designed based on advanced fluid dynamics principles. This allows for better flow distribution and separation efficiency. The design also helps to reduce the pressure drop across the separator, saving energy.
- High - Performance Materials: The company uses high - performance materials in the construction of its oil water separators. These materials are resistant to corrosion, wear, and high temperatures, ensuring the long - term reliability of the products.
- Customized Solutions for Different Industries: Sulzer can provide customized oil water separation solutions for different industries. They take into account the specific requirements of each industry, such as the type of oil, the flow rate, and the environmental conditions, to design the most suitable separator.
- After - sales Support: Sulzer offers comprehensive after - sales support, including spare parts supply, maintenance services, and technical training. Their service teams are highly skilled and can quickly respond to customer needs.
8. GEA Group
Company Introduction
GEA Group is a global technology company that specializes in process engineering and equipment manufacturing. In the area of oil water separation, GEA offers a range of innovative solutions.
GEA has a large R & D department that focuses on developing new technologies and improving existing products. They collaborate with industry partners and research institutions to stay at the forefront of technological advancements. The company's manufacturing facilities are spread across the globe, ensuring efficient production and distribution.
Features and Advantages in Oil Water Separation
- Multi - stage Separation Technology: GEA's oil water separators use multi - stage separation technology. This allows for more efficient separation of oil and water, especially for complex oil - water mixtures. The multi - stage design can remove different sizes of oil droplets at different stages, improving the overall separation efficiency.
- Energy - saving Solutions: The company is committed to developing energy - saving oil water separation solutions. Their products are designed to consume less energy while achieving high - performance separation, which helps to reduce operating costs for customers.
- Hygienic Design: In industries such as food and beverage, GEA's oil water separators feature a hygienic design. This ensures that the separated water and oil meet the strict hygiene standards required by these industries.
- Global Service Network: GEA has a global service network that can provide prompt and efficient after - sales service. Customers can get technical support, spare parts, and maintenance services in a timely manner, ensuring the continuous operation of their oil water separators.
9. Dover Corporation
Company Introduction
Dover Corporation is a diversified global manufacturer with a wide range of products and services. In the field of oil water separation, Dover offers innovative solutions through its various business units.
Dover has a strong R & D culture, investing in new technologies and product development. Their R & D teams work on improving the performance and functionality of their oil water separators. The company also has a well - established quality control system to ensure the reliability of its products.
Features and Advantages in Oil Water Separation
- Innovative Engineering Solutions: Dover's oil water separators are based on innovative engineering solutions. They use advanced materials and design concepts to improve the separation efficiency and durability of the products. For example, some of their separators use unique internal structures to enhance the separation process.
- Flexible Configuration: The company offers flexible configuration options for its oil water separators. Customers can choose different sizes, capacities, and features according to their specific needs. This allows for a more customized solution for different applications.
- Industry - Specific Solutions: Dover can provide industry - specific oil water separation solutions. They understand the unique requirements of different industries, such as the oil and gas industry, the automotive industry, and the chemical industry, and can design products that meet these specific needs.
- Long - term Support: Dover provides long - term support for its products. They offer spare parts, maintenance services, and technical upgrades to ensure the continuous operation and performance improvement of the oil water separators.
10. Schlumberger
Company Introduction
Schlumberger is a leading global provider of technology for the energy industry. In the area of oil water separation, Schlumberger offers advanced solutions that are specifically designed for the oil and gas sector.
Schlumberger has a large - scale R & D organization that focuses on developing cutting - edge technologies for the energy industry. They invest heavily in research to improve the efficiency and performance of their oil water separation products. The company's manufacturing and service operations are spread across the globe, allowing them to serve customers in different regions.
Features and Advantages in Oil Water Separation
- Industry - Specific Expertise: Schlumberger has in - depth industry - specific expertise in the oil and gas sector. Their oil water separators are designed to handle the unique challenges of this industry, such as high - pressure and high - temperature conditions, and the presence of complex oil - water mixtures.
- Advanced Monitoring and Control Systems: The company's oil water separators are equipped with advanced monitoring and control systems. These systems can provide real - time data on the separation process, allowing for better control and optimization of the system.
- Integration with Oilfield Operations: Schlumberger's oil water separation solutions can be integrated with other oilfield operations. This allows for a more seamless and efficient overall production process, reducing costs and improving productivity.
- Sustainable Solutions: Schlumberger is committed to developing sustainable oil water separation solutions. Their products are designed to minimize the environmental impact and comply with strict environmental regulations.
Conclusion
The above - mentioned 10 companies are among the best oil water separator suppliers in the world in 2026. Each company has its own unique features and advantages in the field of oil water separation. Jinhua Shenzhou Centrifuge Co., Ltd. offers high - efficiency and customizable centrifugal separators. Alfa Laval is known for its advanced coalescing technology and wide - range applications. Andritz provides integrated solutions and high - capacity separation. Pall Corporation offers advanced filtration media and modular design. Parker Hannifin features innovative design and versatile applications. Siemens provides intelligent control systems and digital twin technology. Sulzer offers advanced fluid dynamics design and customized solutions. GEA Group uses multi - stage separation technology and energy - saving solutions. Dover Corporation provides innovative engineering solutions and flexible configuration. Schlumberger offers industry - specific expertise and integration with oilfield operations.
These companies play a crucial role in meeting the global demand for oil water separation. Their continuous innovation and development in technology will further improve the efficiency and performance of oil water separators, contributing to environmental protection and the sustainable development of various industries. As the demand for clean water and environmental protection continues to grow, these suppliers will continue to play an important role in the market.