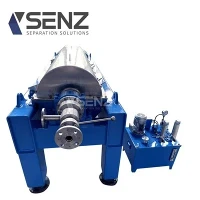

Introduction to 3 Phase Centrifuge
A 3 - phase centrifuge is a highly efficient separation equipment widely used in various industries. It operates based on the principle of centrifugal force to separate different components in a mixture. The "3 - phase" refers to its ability to separate a mixture into three distinct phases, typically a solid phase, a light liquid phase, and a heavy liquid phase. This separation process is crucial in industries such as oil and gas, food and beverage, chemical, and wastewater treatment. In the oil and gas industry, for example, 3 - phase centrifuges are used to separate oil, water, and solids from drilling muds, which helps in recycling valuable drilling fluids and reducing environmental impact. In the food industry, they can separate cream, skim milk, and solids from whole milk, ensuring high - quality product output.
1. Jinhua Shenzhou Centrifuge Co., Ltd.
Company Introduction
Jinhua Shenzhou Centrifuge Co., Ltd. is a well - known player in the centrifuge manufacturing industry. The company has been dedicated to the research, development, production, and sales of centrifuges for many years. With a strong R & D team, they continuously innovate and improve their products to meet the changing needs of different industries. Their production facilities are equipped with advanced manufacturing technologies and equipment, ensuring high - quality product production. The company adheres to strict quality control systems, from raw material procurement to the final product inspection, to ensure that each centrifuge leaving the factory meets international quality standards.
Features in 3 - Phase Centrifuge
- High - Precision Separation: Their 3 - phase centrifuges are designed to achieve high - precision separation of different phases. The unique bowl design and advanced control system ensure that the solid, light liquid, and heavy liquid phases can be separated clearly, with a high degree of separation efficiency.
- Customization: Jinhua Shenzhou Centrifuge Co., Ltd. understands that different industries have different requirements for 3 - phase centrifuges. Therefore, they offer customized solutions according to the specific needs of customers, such as different processing capacities, separation accuracies, and material requirements.
- Energy - Saving Design: In response to the global trend of energy conservation, their 3 - phase centrifuges are designed with energy - saving features. The optimized motor and transmission system reduce energy consumption during operation, which not only saves costs for customers but also conforms to environmental protection requirements.
Company Advantages
- Technical Expertise: The company has a group of experienced engineers and technicians who have in - depth knowledge of centrifuge technology. They can provide professional technical support and solutions to customers, whether it is pre - sales consultation or after - sales service.
- Good Reputation: Over the years, Jinhua Shenzhou Centrifuge Co., Ltd. has established a good reputation in the market. Their high - quality products and excellent service have won the trust and praise of many customers at home and abroad.
- Comprehensive Service: They offer comprehensive services including installation, commissioning, training, and maintenance. Customers can rest assured that they will receive all - around support throughout the life cycle of the centrifuge.
Website
https://www.senz-separation.com/
2. Alfa Laval
Company Introduction
Alfa Laval is a global leader in heat transfer, centrifugal separation, and fluid handling. With a history dating back over 130 years, the company has a long - standing reputation for innovation and quality. It operates in more than 100 countries and has a large number of manufacturing plants and R & D centers around the world. Alfa Laval's products are used in a wide range of industries, including marine, energy, food, and pharmaceuticals. The company is committed to sustainable development and aims to help its customers improve efficiency, reduce environmental impact, and increase profitability.
Features in 3 - Phase Centrifuge
- Advanced Technology: Alfa Laval's 3 - phase centrifuges incorporate the latest technological advancements. Their centrifuges use sophisticated control systems to optimize the separation process in real - time, ensuring consistent and high - quality separation results.
- Robust Design: The centrifuges are built with high - quality materials and a robust design, which can withstand harsh operating conditions. This makes them suitable for use in industries such as offshore oil and gas production, where reliability is of utmost importance.
- High - Capacity Processing: They offer 3 - phase centrifuges with large processing capacities, which can handle high - volume mixtures efficiently. This is beneficial for large - scale industrial applications, such as large - scale food processing plants or oil refineries.
Company Advantages
- Global Presence: With its extensive global network, Alfa Laval can provide prompt and efficient service to customers around the world. Whether it is technical support, spare parts supply, or after - sales service, customers can rely on the company's local teams.
- Research and Development: The company invests heavily in research and development. This allows them to continuously improve their products and develop new technologies, keeping them at the forefront of the centrifuge industry.
- Industry Experience: Alfa Laval has decades of experience in the centrifuge industry. They have a deep understanding of different industries' needs and can provide customized solutions based on this knowledge.
3. GEA Group
Company Introduction
GEA Group is a global technology company that specializes in process engineering and equipment manufacturing. It has a wide range of products and services, including 3 - phase centrifuges. The company serves various industries such as food and beverage, chemical, and pharmaceutical. GEA has a strong focus on innovation and sustainability, aiming to develop solutions that improve the efficiency and environmental performance of its customers' processes. With a large team of engineers and researchers, GEA is constantly exploring new technologies and materials to enhance the performance of its products.
Features in 3 - Phase Centrifuge
- Integrated Solutions: GEA offers integrated 3 - phase centrifuge solutions that can be easily integrated into existing production lines. This includes not only the centrifuge itself but also related control systems and accessories, which simplifies the installation and operation process for customers.
- Hygienic Design: In industries such as food and pharmaceuticals, hygiene is a critical factor. GEA's 3 - phase centrifuges are designed with hygienic features, such as smooth surfaces, easy - to - clean components, and compliance with strict hygiene standards.
- Process Optimization: The company's centrifuges are designed to optimize the separation process. They use advanced algorithms and sensors to monitor and adjust the operating parameters in real - time, ensuring the best possible separation results with minimal energy consumption.
Company Advantages
- Multidisciplinary Expertise: GEA has expertise in multiple disciplines, including mechanical engineering, chemical engineering, and automation. This allows them to provide comprehensive solutions that take into account all aspects of the separation process.
- Quality Assurance: GEA has a strict quality assurance system in place. From the design phase to the final product delivery, every step is carefully monitored to ensure that the 3 - phase centrifuges meet the highest quality standards.
- Long - Term Partnerships: The company has established long - term partnerships with many customers around the world. This is a testament to its reliable products, excellent service, and commitment to customer satisfaction.
4. Andritz AG
Company Introduction
Andritz AG is an international technology group that operates in the fields of hydropower, pulp and paper, metalworking, and separation technology. In the area of separation technology, Andritz has a strong presence in the 3 - phase centrifuge market. The company has a global network of production and sales facilities, serving customers in more than 40 countries. Andritz is known for its high - tech products and innovative solutions, which are designed to improve the productivity and efficiency of its customers' operations.
Features in 3 - Phase Centrifuge
- Modular Design: Andritz's 3 - phase centrifuges feature a modular design, which allows for easy customization and expansion. Customers can choose different modules according to their specific needs, such as different bowl sizes, feed systems, and discharge mechanisms.
- High - Speed Separation: The centrifuges are capable of high - speed operation, which results in faster separation times and higher throughput. This is particularly beneficial for industries with high - volume production requirements.
- Remote Monitoring and Control: Andritz offers 3 - phase centrifuges with remote monitoring and control capabilities. Customers can monitor the operation status of the centrifuge in real - time and make adjustments from a remote location, which improves operational efficiency and reduces the need for on - site personnel.
Company Advantages
- Engineering Excellence: The company has a team of highly skilled engineers who are experts in separation technology. They can provide in - depth technical support and design customized solutions for customers.
- After - Sales Service: Andritz provides comprehensive after - sales service, including maintenance, repair, and spare parts supply. Their global service network ensures that customers can get prompt assistance whenever they need it.
- Sustainable Solutions: Andritz is committed to developing sustainable solutions. Their 3 - phase centrifuges are designed to reduce energy consumption and waste generation, which helps customers meet their environmental goals.
5. Flottweg SE
Company Introduction
Flottweg SE is a German - based company that specializes in the development, production, and sale of centrifuges and decanters. The company has a long history of innovation in the centrifuge industry and is known for its high - quality products. Flottweg serves a wide range of industries, including the chemical, pharmaceutical, and food industries. It has a strong focus on customer - oriented solutions, working closely with customers to understand their needs and develop the most suitable products.
Features in 3 - Phase Centrifuge
- Intelligent Control System: Flottweg's 3 - phase centrifuges are equipped with an intelligent control system. This system can automatically adjust the operating parameters according to the properties of the input mixture, ensuring optimal separation results.
- Low - Maintenance Design: The centrifuges are designed with low - maintenance features, such as long - lasting bearings and easy - to - access components. This reduces the downtime and maintenance costs for customers.
- High - Quality Construction: Flottweg uses high - quality materials and advanced manufacturing processes to build its 3 - phase centrifuges. This results in a durable and reliable product that can operate continuously for long periods.
Company Advantages
- German Engineering: As a German company, Flottweg benefits from the reputation of German engineering for precision and quality. Their products are known for their high performance and reliability.
- Customer - Centric Approach: The company places a strong emphasis on customer satisfaction. They work closely with customers from the initial consultation to the final commissioning of the centrifuge, providing personalized solutions and support.
- Global Service Network: Flottweg has a global service network, which enables them to provide fast and efficient service to customers around the world. Whether it is for installation, maintenance, or repair, customers can rely on their local service teams.
6. Rousselet Robatel
Company Introduction
Rousselet Robatel is a French company that has been specializing in centrifuge technology for over 150 years. It is a leading manufacturer of centrifuges for various industries, including the food, chemical, and pharmaceutical sectors. The company has a strong tradition of innovation and quality, and its products are known for their high performance and reliability. Rousselet Robatel has a global presence, with sales and service offices in many countries around the world.
Features in 3 - Phase Centrifuge
- Unique Bowl Design: The 3 - phase centrifuges of Rousselet Robatel feature a unique bowl design that enhances the separation efficiency. The design allows for better distribution of the mixture inside the centrifuge, resulting in more accurate separation of the three phases.
- Sanitary Design: In industries where hygiene is crucial, such as the food and pharmaceutical industries, Rousselet Robatel's centrifuges are designed with sanitary features. They are easy to clean and disinfect, ensuring compliance with strict hygiene standards.
- Flexible Operation: The centrifuges can be operated in a flexible manner, allowing for different processing modes and adjustment of operating parameters. This makes them suitable for a wide range of applications and different types of mixtures.
Company Advantages
- Long - Standing Experience: With over 150 years of experience in the centrifuge industry, Rousselet Robatel has in - depth knowledge and expertise. They can draw on this experience to develop the best solutions for their customers.
- French Craftsmanship: The company is known for its French craftsmanship, which is reflected in the high - quality construction and attention to detail of its products.
- Technical Support: Rousselet Robatel provides comprehensive technical support to its customers. Their team of experts can assist customers in the selection, installation, and operation of the 3 - phase centrifuges.
7. Westfalia Separator Group
Company Introduction
Westfalia Separator Group is a well - established company in the field of separation technology. It offers a wide range of centrifuges, including 3 - phase centrifuges, for various industries such as oil and gas, food, and chemical. The company has a global presence, with production facilities and sales offices in many countries. Westfalia Separator Group is committed to providing high - quality products and excellent service to its customers, and it continuously invests in research and development to improve its product offerings.
Features in 3 - Phase Centrifuge
- High - Performance Separation: The 3 - phase centrifuges of Westfalia Separator Group are designed to achieve high - performance separation. They can handle difficult - to - separate mixtures and provide clear separation of the solid, light liquid, and heavy liquid phases.
- Automated Operation: The centrifuges are equipped with advanced automation systems, which can control the entire separation process automatically. This reduces the need for manual intervention and improves the consistency of the separation results.
- Energy - Efficient Design: Westfalia Separator Group pays attention to energy efficiency in the design of its 3 - phase centrifuges. The use of advanced motor technology and optimized hydraulic systems helps to reduce energy consumption during operation.
Company Advantages
- Industry Leadership: The company is a leader in the separation technology industry. Its long - standing reputation and extensive experience give it an edge in the market.
- Comprehensive Product Range: Westfalia Separator Group offers a comprehensive range of 3 - phase centrifuges with different capacities and specifications. This allows customers to choose the most suitable product for their specific needs.
- Global Service and Support: With its global service network, the company can provide prompt and efficient service to customers around the world. This includes installation, maintenance, and technical support.
8. Heinkel Drying and Separation Group
Company Introduction
Heinkel Drying and Separation Group is a leading provider of separation and drying technology. The company has a wide range of products, including 3 - phase centrifuges, which are used in industries such as chemical, pharmaceutical, and food. Heinkel has a strong focus on innovation and quality, and it invests in research and development to develop new and improved products. The company has production facilities in several countries and serves customers around the world.
Features in 3 - Phase Centrifuge
- Integrated Drying Function: Some of Heinkel's 3 - phase centrifuges are equipped with an integrated drying function. This allows for the simultaneous separation and drying of the solid phase, which is particularly useful in industries where dry solids are required.
- Advanced Material Handling: The centrifuges are designed with advanced material handling systems, which ensure smooth and efficient feeding and discharge of the mixture. This reduces the risk of blockages and improves the overall performance of the centrifuge.
- Custom - Built Solutions: Heinkel offers custom - built 3 - phase centrifuge solutions according to the specific requirements of customers. They can design and manufacture centrifuges with special features and specifications to meet the unique needs of different industries.
Company Advantages
- Technical Innovation: The company is at the forefront of technical innovation in the separation and drying technology field. Their continuous investment in R & D allows them to develop cutting - edge products.
- Quality Manufacturing: Heinkel has strict quality control measures in place during the manufacturing process. This ensures that their 3 - phase centrifuges are of high quality and reliable.
- Customer - Focused Service: Heinkel provides customer - focused service, from the initial project planning to the after - sales support. They work closely with customers to ensure that their needs are met throughout the life cycle of the centrifuge.
9. Bird Technologies
Company Introduction
Bird Technologies is a well - known company in the centrifuge industry. It has been manufacturing centrifuges for a long time and has a wide customer base in different industries. The company is committed to providing innovative and reliable separation solutions. Bird Technologies has a team of experienced engineers and technicians who are dedicated to product development and improvement.
Features in 3 - Phase Centrifuge
- Advanced Separation Technology: Bird Technologies' 3 - phase centrifuges incorporate advanced separation technology. Their unique design ensures efficient separation of the three phases, even for mixtures with complex properties.
- User - Friendly Interface: The centrifuges are equipped with a user - friendly interface, which makes it easy for operators to control and monitor the centrifuge. This reduces the training time required for new operators and improves the overall operational efficiency.
- Cost - Effective Solutions: The company offers cost - effective 3 - phase centrifuge solutions. They strive to provide high - quality products at a reasonable price, which is attractive to customers with budget constraints.
Company Advantages
- Proven Track Record: Bird Technologies has a proven track record in the centrifuge industry. Their products have been widely used and have received positive feedback from customers.
- Technical Support: The company provides comprehensive technical support to its customers. Whether it is troubleshooting or product improvement, their technical team is always available to assist.
- Continuous Improvement: Bird Technologies is committed to continuous improvement. They regularly update their products based on customer feedback and technological advancements, ensuring that their 3 - phase centrifuges remain competitive in the market.
10. Sharples (a part of Alfa Laval)
Company Introduction
Sharples, now a part of Alfa Laval, has a long - standing history in the centrifuge industry. It was a pioneer in the development of centrifuge technology and has a reputation for high - quality products. Sharples' products are used in a wide range of industries, including oil and gas, chemical, and food. As part of Alfa Laval, Sharples benefits from the global resources and technological expertise of the larger group.
Features in 3 - Phase Centrifuge
- Heritage of Innovation: Sharples has a heritage of innovation in centrifuge technology. Their 3 - phase centrifuges incorporate the latest advancements based on decades of research and development.
- Compatibility with Alfa Laval Ecosystem: As part of Alfa Laval, Sharples' 3 - phase centrifuges can be easily integrated with other Alfa Laval products and systems. This allows for seamless operation and enhanced performance in a larger process environment.
- Reliable Performance: The centrifuges are known for their reliable performance. They are built to withstand continuous operation and can handle a wide range of operating conditions.
Company Advantages
- Alfa Laval Synergy: The synergy with Alfa Laval provides Sharples with access to a larger pool of resources, including research and development, manufacturing, and global sales and service networks.
- Brand Reputation: Sharples has a well - established brand reputation in the centrifuge industry. Customers trust the quality and performance of their products.
- Comprehensive Product Portfolio: In combination with Alfa Laval, Sharples offers a comprehensive product portfolio, which can meet the diverse needs of different industries.
Conclusion
The above - mentioned 10 companies are leading players in the 3 - phase centrifuge factory in the world. Each company has its own unique features and advantages in the production of 3 - phase centrifuges. Some are known for their advanced technology and innovation, such as Alfa Laval and GEA Group; others are recognized for their long - standing experience and high - quality craftsmanship, like Rousselet Robatel and Sharples. The ability to provide customized solutions, energy - efficient designs, and comprehensive after - sales service is also a common strength among these companies. As industries continue to develop and demand more efficient and reliable separation solutions, these leading 3 - phase centrifuge factories will likely continue to innovate and play a crucial role in meeting the needs of various sectors around the world. Whether it is for large - scale industrial applications or specialized niche industries, customers can choose the most suitable 3 - phase centrifuge manufacturer based on their specific requirements.